Oil & Gas
and Petrochemical

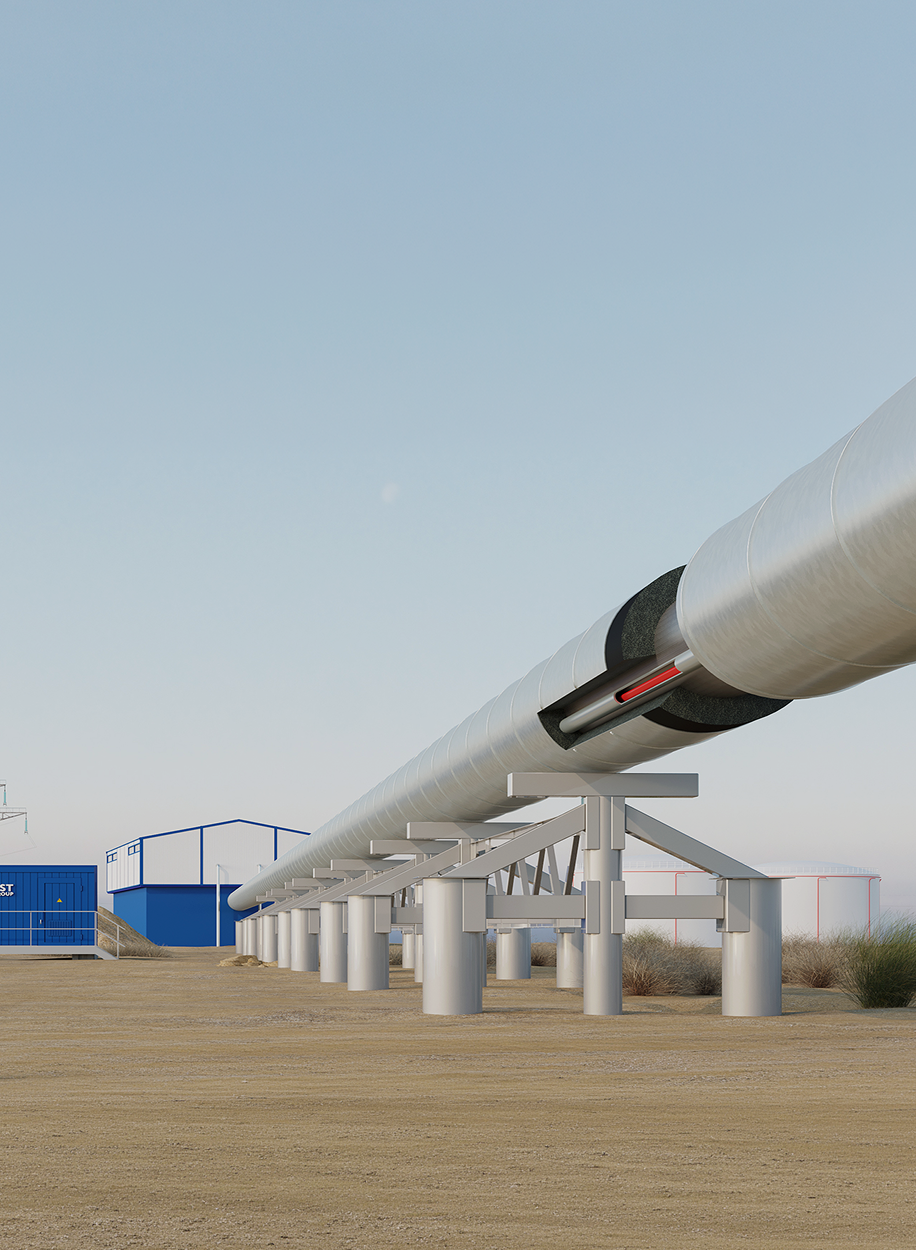
Sigmian delivers complete electric heat tracing systems for upstream, midstream and downstream oil & gas facilities, petrochemical plants and refineries. Our solutions ensure reliable process temperature maintenance, freeze protection and safe operation in hazardous environments.
Advantages
Process equipment
Reliable
Freeze Protection
of critical process equipment
Reduced
maintenance
and operational costs
Accurate process
temperature maintenance
Energy-efficient
self-regulating heating technology
Safe operation
in hazardous (Ex) areas
Increased process reliability
and plant uptime
Complete engineered systems
from design to commissioning
Suitable for new construction
and retrofit projects
Typical Applications
Process
pipelines
Storage
tanks
Pumps
Pumps
Instrumentation
Fuel and chemical transfer lines
Offshore
modules
Process
vessels

Applications
Across The Industry

Sigmian heat tracing systems are designed for the demanding requirements of oil & gas and petrochemical facilities, including:
Refineries
Petrochemical
plants
LNG
terminals
Gas processing
facilities
Oil storage
terminals
Pipeline
infrastructure
Offshore
platforms
Chemical
processing plants
Our Projects

Integrated Electricity and Water Plant in Duqm, Oman

View the project
Integrated Electricity and Water Plant in Duqm, Oman

Port of Fujairah Terminals, UAE

View the project
Port of Fujairah Terminals, UAE

Integrated Electricity and Water Plant in Duqm, Oman

View the project
Integrated Electricity and Water Plant in Duqm, Oman

Port of Fujairah Terminals, UAE

View the project
Port of Fujairah Terminals, UAE

SEHT system for 8" Dia extract oil pipeline CPCL

View the project
SEHT system for 8" Dia extract oil pipeline CPCL

Kumho Mitsui Chemicals Plant

View the project
Kumho Mitsui Chemicals Plant
Operating Principle
Electric heat tracing system1234567
1Heating cable
2Thermal insulation
3Pipe / Vessel
4Junction box
5Power cable
6Temperature sensor
7Control panel

How Electric
Heat Tracing Works

Electric heat tracing systems compensate for heat losses from pipes, tanks and process equipment to maintain the required operating temperature or provide freeze protection.

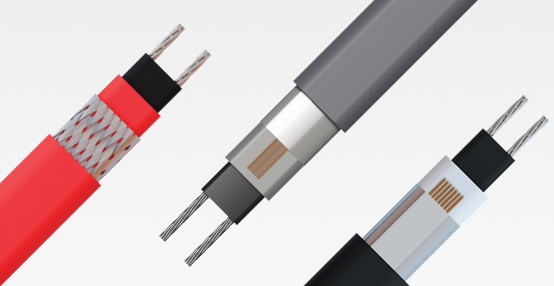
Depending on the application, self-regulating, constant wattage or mineral insulated heating cables are selected to achieve the required performance under the site’s environmental and process conditions. Heating cables are installed directly on the equipment surface beneath thermal insulation.

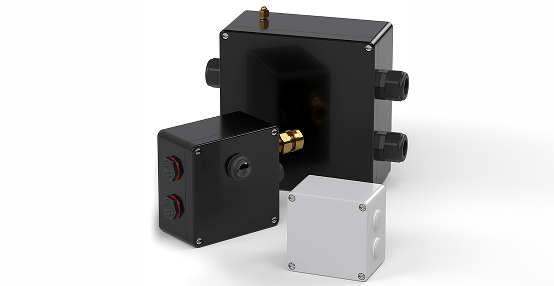
The system is connected through certified junction boxes and controlled by dedicated temperature control panels to ensure safe, reliable and energy-efficient operation. For high-temperature processes and chemically aggressive environments, Sigmian also offers mineral insulated heating cables capable of operating at temperatures up to 800°C.

Each heat tracing system is individually engineered based on process temperature, ambient conditions, insulation design, hazardous area classification and project requirements.

Why Choose Sigmian
Complete
Engineered
heat tracing systems
Certified
Solutions
for hazardous areas
International
Project
Experience
Long-Term
Operational
Reliability
Wide
Portfolio
of heating cable
technologies
Custom
Solutions
for complex
industrial facilities
Engineering
Support
from concept
to commissioning
Reliable
Supply
of components
and accessories
Approvals
CE
Atex
Recommended Products
Contacts